TIG Welding GCD-level Options
The MIG Welding operation provides the following options, which can be set on a per-GCD basis:
Weld Cycle Time Method
Arc time is the time for the arcing phase of welding—it excludes arc time for tack welding. Arc time is determined in one of two ways:
-
Volumetric Rate Method: based on the following:
-
Weld volume
-
Deposition rate (derived from the machine property Wire Feed Rate and an estimate of wire diameter)
-
-
Linear Rate Method: based on the following:
-
Weld length
-
See the formulas for Volume Method Arc Time Calculated and Length Method Arc Time Calculated in TIG Welding Operation Weld Time.
Assembly Material Type
By default in starting point Digital Factories, the weld is assumed to use Steel filler. Administrators can customize the default with the cost model variable defaultTigWeldingMaterialType. Users can override the default filler type on a part-by-part basis with this setup option. Select from the dropdown list, (which is populated from the Material Type column of the lookup table tblTigWelding).
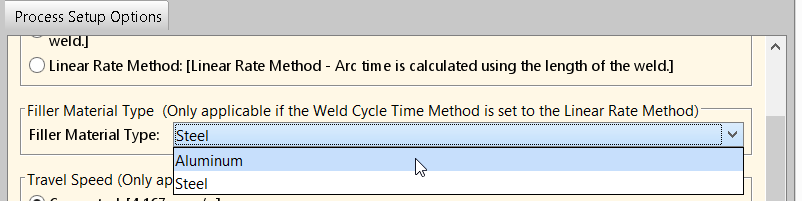
Filler material type affects travel speed, which affects TIG Welding Operation Weld Time, if the Linear Rate Weld Cycle Time Method is enabled. It also affects TIG Welding Weld Weight and the TIG Welding Expendable Tooling Calculation.
Assembly Position
This specifies the position of the assembly during welding:
-
Flat: the weld head is held above the weld.
-
Horizontal/vertical: the weld head is held at the same height as the weld.
-
Overhead: the weld head is held below the weld.
By default in starting point Digital Factories, the assembly position is assumed to be Flat. Users can override the default position on a part-by-part basis with this setup option. Select from the dropdown list, (which is populated from the Position column of the lookup table tblTigWelding).
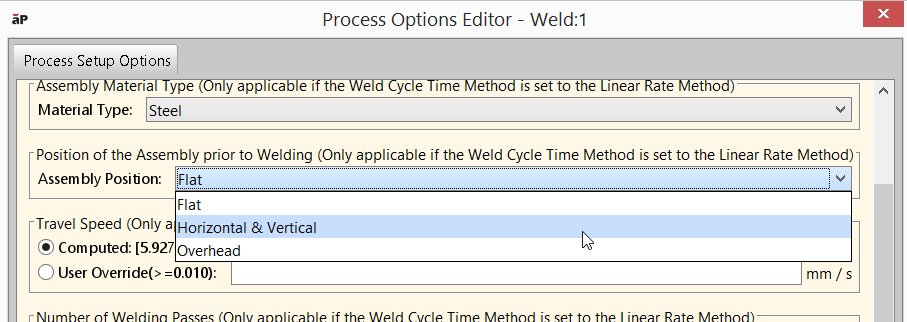
Assembly position affects travel speed, which affects TIG Welding Operation Weld Time, if the Linear Rate Weld Cycle Time Method is enabled.
Travel Speed
If the Linear Rate Weld Cycle Time Method is used, weld time is based, in part, on travel speed; see TIG Welding Operation Weld Time. This is the speed (distance per unit time) at which the weld head travels along the length of the weld.
By default, it is looked up in the lookup table tblTigWeldingV2 by the following:
- Weld Throat for a Canonical Weld that is equivalent to the portion of the weld created in a single pass. This is the throat for a Canonical Weld whose area equals the following: the Weld Cross-sectional Area of the current weld divided by the Number of Welding Passes.
- Assembly Material Type
If the Assembly Position is Horizontal or Overhead, the looked up value is adjusted by multiplying it by the value of one of the following cost model variables:
- Horizontal: tigWeldHorizontalSpeedMultiplier (0.85 in starting point Digital Factories)
- Overhead: tigWeldOverheadSpeedMultiplier (0.7225 in starting point Digital Factories)
Users can override the default on a per-GCD basis with the setup option Travel Speed.
Number of Welding Passes
If the linear rate Weld Cycle Time Method is used, weld time is based, in part, on the number of welding passes used for weld (that is, the number of times the weld head traverses the length of the weld). By default, the number of welding passes is looked up in the lookup table tblNumWeldPasses by the following:
- Process type (MIG or TIG)
- Weld Throat of a Canonical Weld with the same area as the current weld.
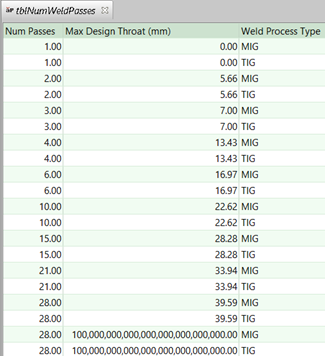
Users can override the default on a per-GCD basis with the setup option Number of Welding Passes.
Gas Type used for Welding
By default, the type of gas used for welding is specified by the cost model variable defaultTigWeldingGasType (Argon in starting point Digital Factories). Users can override the default with this setup option. Gas type affects gas cost; see Additional Direct Costs for TIG Welding.
Enable Anti-Spatter Spray
By default in starting point Digital Factories, costs for antispatter spray are included in expendable tooling costs; see TIG Welding Expendable Tooling Calculation. Administrators can customize the default, and specify no cost for antisplatter spray, by setting the cost model variable weldAntiSpatterSprayEnabled to false. Users can override the default on a per weld basis with this setup option.
Number of Welder Positions
For robotic welding, the cost model accounts for the time for the welder to position itself once per Weld GCD. For manual welding, the cost model estimates the number of welder positions based on the number of weld segments, the segment length, and the machine property Welder Reach--see Manual TIG Welding and Robotic TIG Welding.
With the setup option Number of Welder Positions, the user can override the default on a per-GCD basis. The number of welder positions drives welding cycle time and labor time.